
In the injection molding process, the plastic mold design phase sets the budget and delivery schedule for the entire project. An incomplete engineering drawing does not merely mean minor CAD adjustments on screen; it leads to severe, costly overhead: molds must be disassembled for repeated secondary machining, defect scrap rates rise, and molding cycle times stretch longer. Identifying common engineering calculation mistakes early is a direct way for enterprises to safeguard capital and maintain consistent finished component quality.
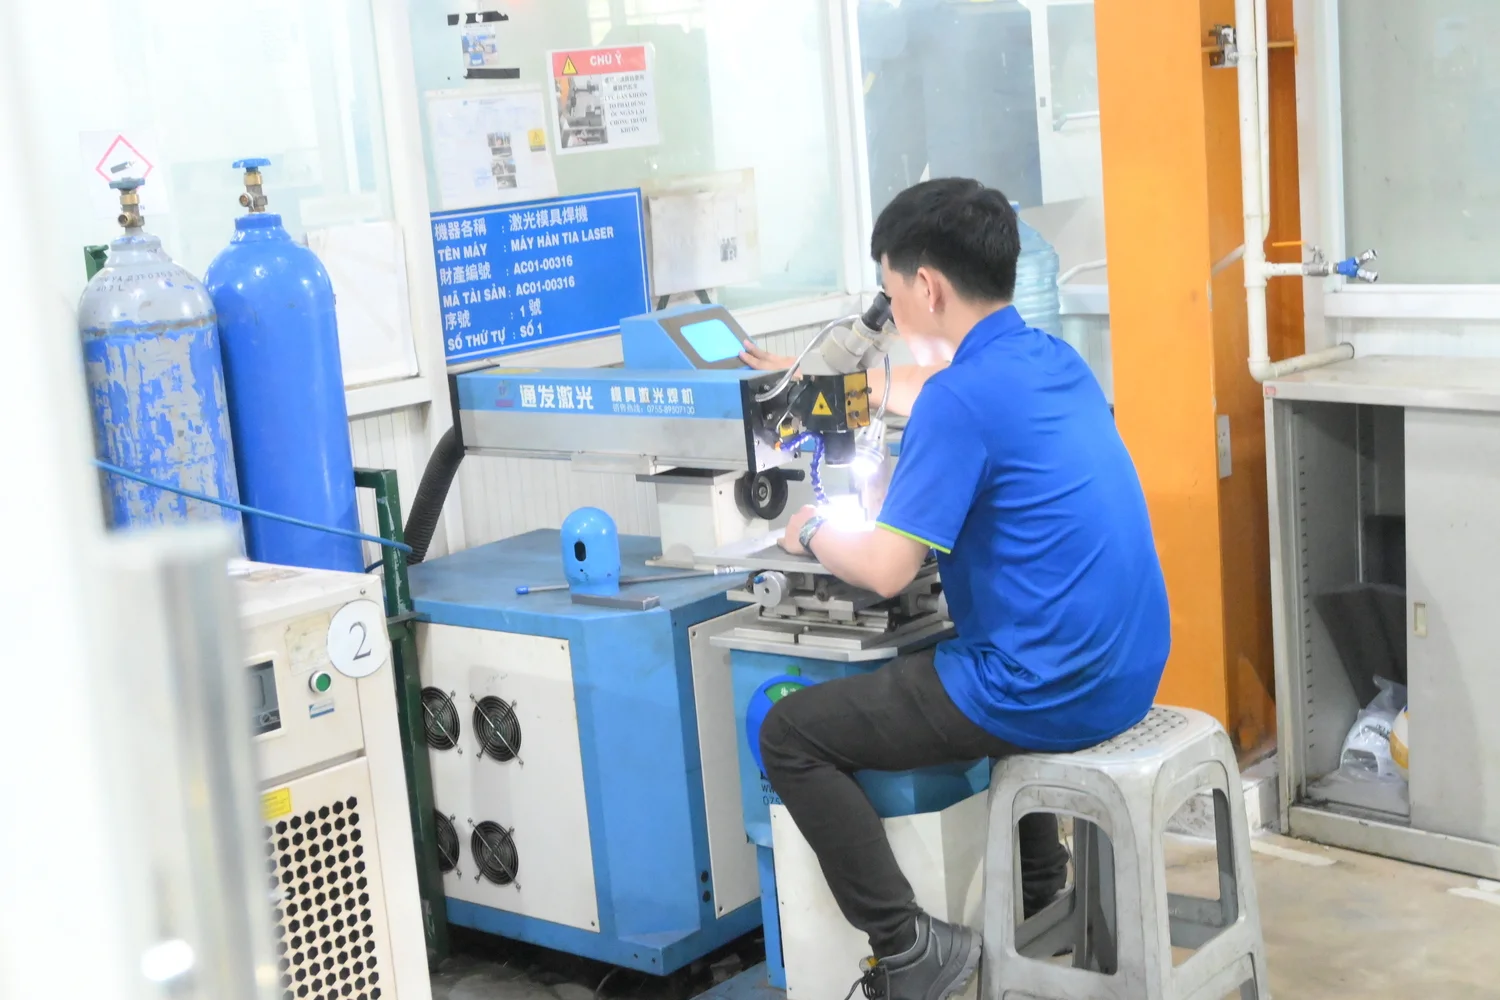
Ignoring draft angles and the consequences of parts sticking in cavities
The draft angle is the necessary taper applied to vertical part walls parallel to the mold opening and closing direction. This geometric feature ensures that releasing molded parts from core and cavity steel surfaces proceeds smoothly once the ejector pin system actuates.
When engineers omit or specify inadequate draft angles (below the standard 1° – 2° guideline depending on resin chemistry), friction between the contracting plastic skin and tool steel walls increases dramatically. This induces direct engineering failures:
• Molded parts develop drag scratches: Along cosmetic surfaces or suffer mechanical buckling distortion under excessive ejector pin punch force.
• Elevated demolding drag: Places severe bending stresses on ejector pins, causing premature pin bending or fracture, galling internal cavity walls, and shortening mechanical tooling life.
The financial penalty appears immediately on the shop floor: presses experience continuous machine downtime as technicians manually pry stuck moldings out of the tool. To remediate this, enterprises are forced to pull the mold for rework via sinker EDM or CNC milling to widen draft angles. Secondary machining expenses combined with idle machine downtime substantially inflate final piece-part costs.
Non-uniform wall thickness causing warpage and extending cycle times
A fundamental yet frequently overlooked principle in plastic mold design is maintaining uniform nominal wall thickness across the component. Molten resin injected into cavity steel solidifies from the outside inward; thick wall sections retain heat far longer than adjacent thin walls, generating large disparities in volumetric shrinkage rates.
Non-uniform wall thickness routinely triggers two severe cosmetic and physical defects:
• Surface sink marks: Typically form at oversized screw boss roots or reinforcing rib intersections where bulky interior cores shrink inward, pulling exterior aesthetic surfaces down as they cool.
• Warpage: Differential shrinkage rates across adjacent zones on the same component produce internal residual stresses, distorting part geometry once ejected from cavity steel.
Financially, to mitigate sink marks on thick sections, process technicians are forced to lengthen cooling cycles and prolong pack-and-hold durations. This substantially lengthens overall cycle times. Extending cycle duration by even 5 to 15 seconds per shot lowers hourly throughput while increasing electrical utility consumption and machine amortization per part proportionally. Furthermore, out-of-spec scrap parts that fail assembly fit-up waste substantial quantities of virgin engineering resin.
Improper gate positioning compromising cosmetic appeal and mechanical structure
The injection gate is the designated orifice directing molten resin from runner channels into the cavity. Gate placement dictates melt front advancement vectors, cavity packing pressures, and venting efficiency across the tool.
Common mistakes in gate location include placing gates within high-stress loading zones, locating them excessively far from thin sections, or positioning them such that melt streams split and re-converge improperly:
• Structurally compromised weld lines: When two cooler melt fronts meet, they form a knit line. If this line forms along structural loading ribs or mechanical snap-fit joints, the component will easily crack or fracture during operational use.
• Unbalanced cavity packing and air traps: An unbalanced melt flow compresses trapped cavity air against dead ends, causing localized burn marks (diesel effect) or short-shot defects where air fails to escape through parting-line vents.
Altering gate locations is an intricate task in precision toolmaking. Once tool steel has undergone hardening heat treatment, rerouting runner paths and shifting gate geometry demands delicate laser welding or replacing core/cavity inserts entirely. Such rework not only incurs substantial mechanical modification costs but also delays critical product launch schedules.
GET THE BEST QUOTE
Contact ZENG HSING now via Zalo or Website to receive advice on suitable specifications and get a prompt quotation!
Precision plastic mold design solutions at Zeng Hsing
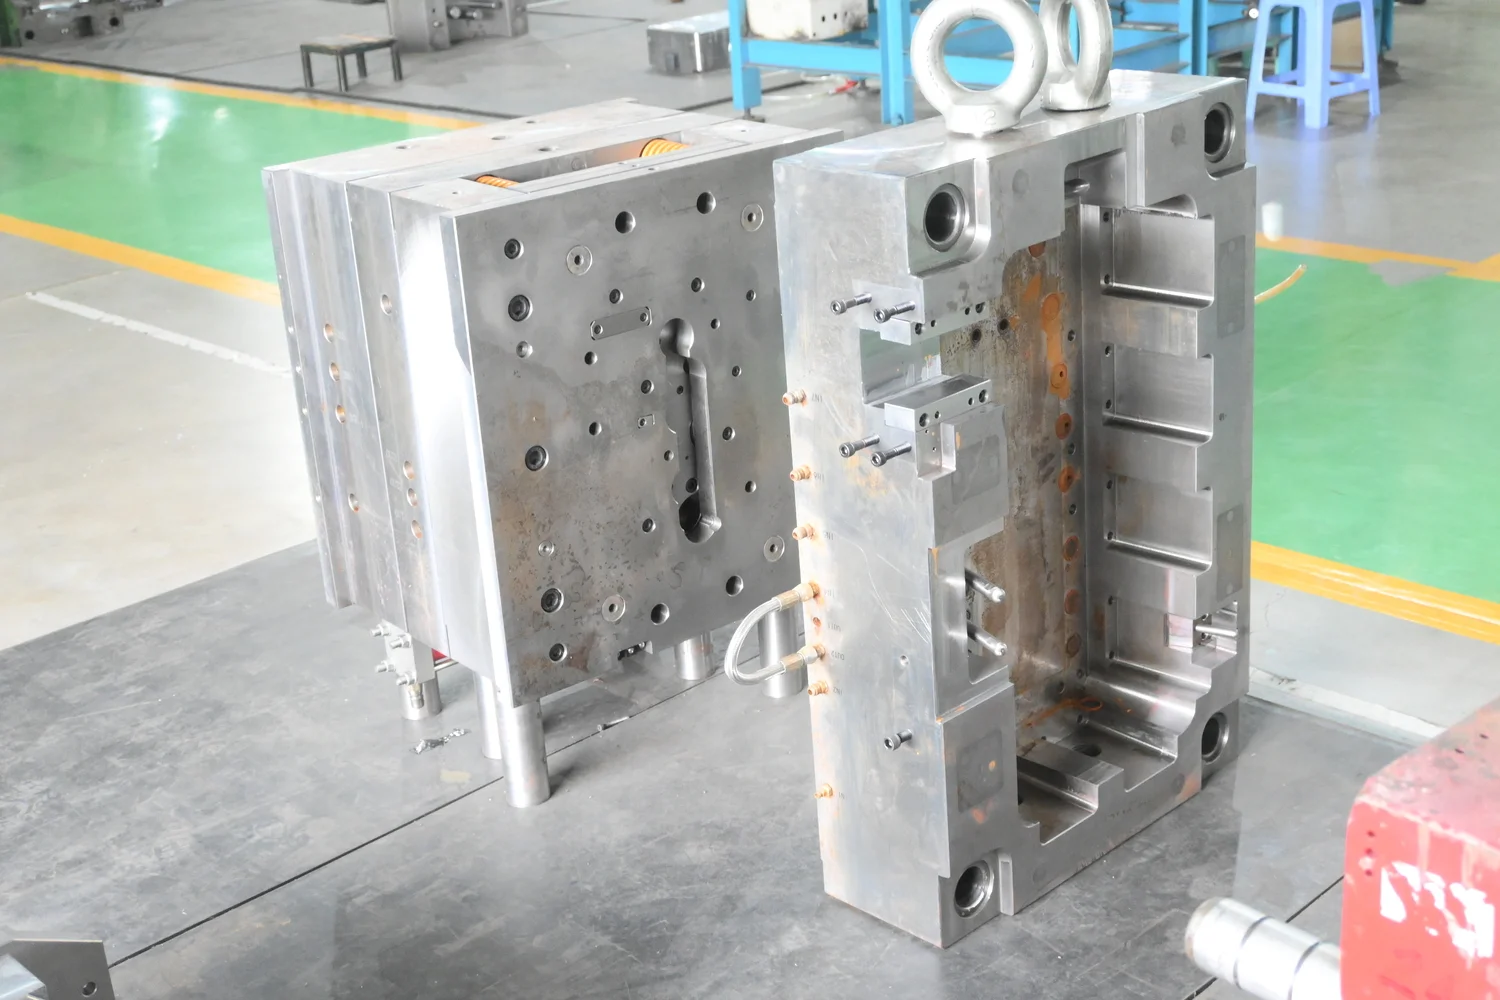
Conducting polymer melt flow simulations and thoroughly auditing draft angles, nominal wall thickness, and gate layouts directly on engineering drawings is a practical solution to control manufacturing budgets. Enterprises can collaborate with the engineering team at Zeng Hsing to carry out comprehensive DFM evaluations, identify potential tool design flaws early, and manufacture durable, high-precision injection molds tailored to project budgets.
ZENG HSING VIET NAM
- Address: Unit 03-08, Canary Plaza, Binh Duong Boulevard, Binh Hoa Ward, Ho Chi Minh City, Vietnam
- Hotline: (+84) 0355 846 965 (Mr. Nghia) – (+84) 0362 476 478 (Mr. Nam)
- Email: nghia_duong@zenghsing.com.vn / nam_vu@zenghsing.com.vn
- Website: zenghsing.vn

